Top 10 Heavy Duty Hydraulic Press Types for Global Buyers
Choosing the right Heavy Duty Hydraulic Press is rarely a simple capacity decision. Global buyers must compare force, stroke length, daylight, bed size, control systems, and working speed. A 1,000-ton press may sound impressive, yet it can fail a buyer’s needs if its frame lacks rigidity or its hydraulic circuit responds slowly. Pressure matters.
This guide examines ten major hydraulic press types used across metal forming, forging, molding, straightening, compaction, and industrial assembly. Each type serves a different production reality. A four-column press offers broad stability for large components, while a C-frame press improves access for smaller workpieces. Deep drawing presses demand controlled movement and accurate blank-holder pressure. Forging presses require exceptional frame strength, reliable pumps, and carefully managed thermal conditions.
The evaluation also considers installation space, energy consumption, maintenance access, operator visibility, tooling compatibility, and after-sales support. These details often determine whether a machine performs well after five years, not just during a factory demonstration. Experienced buyers should request load charts, cycle data, material records, inspection reports, and references from comparable plants. Details matter.
Safety and compliance require equal attention. Buyers should verify guarding, emergency stops, hydraulic hose protection, documentation, and applicable local machinery requirements. ISO-based safety practices can provide useful guidance, but regional rules still require professional review. No ranking can fit every factory. Some recommendations may change when production volume, material thickness, or labor conditions differ. That uncertainty deserves honest discussion, not polished sales language.
Hydraulic Press Fundamentals and Global Market Terminology
Top 10 Heavy Duty Hydraulic Press Types for Global Buyers
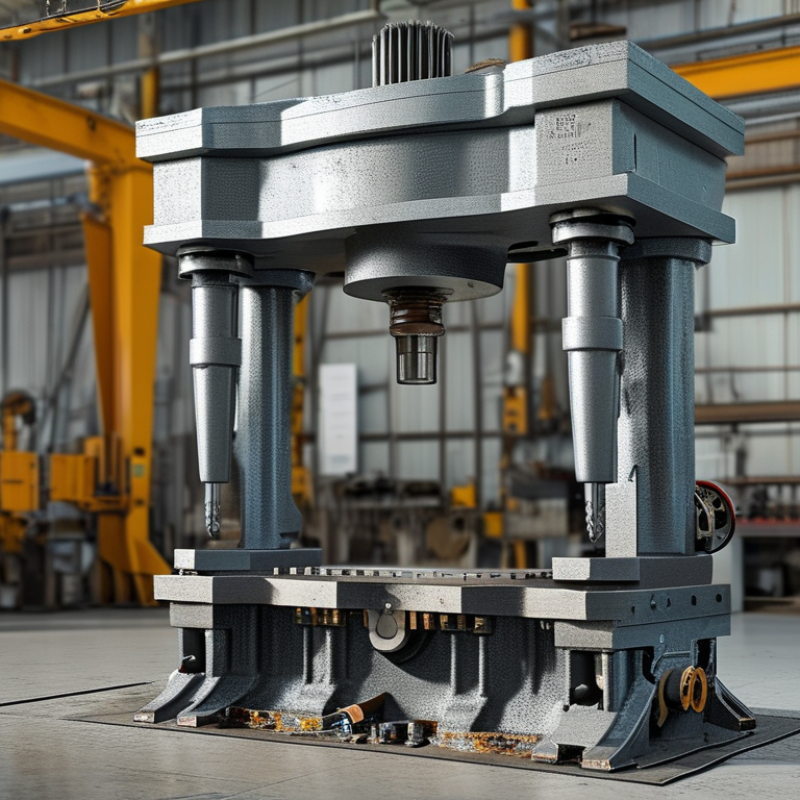
Hydraulic press selection starts with basic terms, not impressive tonnage figures. A press converts hydraulic pressure into ram force through a pump, cylinder, and control system. Tonnage describes maximum force, while working pressure describes the force available within the circuit. They are related, but not identical.
Global quotations often mention daylight, stroke, bed size, throat depth, and approach speed. Daylight is the open space between the bed and ram. Stroke is the ram’s travel distance. Throat depth matters when sheet material must reach deep inside the frame. C-frame, H-frame, four-column, straight-side, and gantry presses suit different loading patterns. Deep-drawing, forging, forming, powder-compacting, briquetting, trimming, and laminating presses require different tooling and control accuracy.
Ask whether the quoted force is nominal or continuous. This detail is easy to miss. Check oil temperature limits, pump flow, pressure-holding performance, die height, and ram guidance. A faster approach stroke may not improve production if return speed remains slow. In my view, buyers sometimes compare motor power too quickly and overlook cycle time. That judgment can be wrong.
Terms such as PLC control, proportional valve, emergency stop, guarding, and overload protection should appear clearly in technical documents. Request drawings, load diagrams, inspection records, and maintenance intervals. Metric dimensions may conflict with inch-based tooling, creating costly surprises. A careful buyer verifies every unit, tolerance, and interface before approving the final specification.
Top 10 Heavy-Duty Hydraulic Press Types for Global Buyers
Representative nominal pressing-force benchmarks for widely used hydraulic press configurations. Values are typical reference points rather than universal limits; actual ratings vary by application, frame design, stroke, and operating standard.
Hydraulic press capacity is commonly specified in metric tonnes or meganewtons. Forging, straight-side, and tire presses generally occupy the highest-capacity segment, while C-frame and laminating presses are commonly selected for lower-force forming and assembly work.
Global Buyer Criteria: Materials, Standards, and Safety Requirements
Selecting a heavy-duty hydraulic press starts with the material, not the catalog photograph. Four-column presses suit deep drawing and forming. C-frame models improve side access for stamping and straightening. H-frame presses handle repair work and flexible tooling. Forging, extrusion, lamination, and rubber-pad operations need different pressure curves and platen designs.
The World Steel Association reported 1,892.2 million tonnes of crude steel production in 2023. That scale exposes a practical issue: steel grades vary widely in yield strength and springback. Buyers should request verified load calculations, platen deflection data, and material certificates. A 1,000-ton rating alone proves little. Fit matters. Check daylight, stroke, bolster thickness, ram alignment, and cycle temperature. ISO 16092-3:2017 addresses safety requirements for hydraulic presses used in metalworking. It should guide technical specifications, not decorate them.
Safety verification must include guarding, emergency stops, two-hand controls, hydraulic hose protection, and safe die access. OSHA 1910.212 requires guarding against machine hazards, while the U.S. Bureau of Labor Statistics recorded 5,283 fatal work injuries in 2023. The number is not press-specific, but it shows why assumptions are expensive. Small gaps matter. Ask for risk assessments, pressure-relief test records, electrical compliance documents, and operator training procedures. Standards may be available, yet installation quality can still fail. A neglected hose, poorly supported die, or rushed commissioning can defeat a well-designed machine. No checklist is perfect. Recheck it on the factory floor.
Comparing Applications, Costs, and Suppliers Across Global Markets
Top 10 Heavy Duty Hydraulic Press Types for Global Buyers
Global buyers should compare application fit before tonnage. The ten common categories include four-column, H-frame, C-frame, forging, extrusion, deep-drawing, straight-side, rubber-pad, hot-forming, and multi-action presses. Four-column machines suit controlled stamping and compression. Forging presses demand rigid frames, high flow, and repeatable pressure. C-frame units cost less, but frame deflection can limit precision. According to Grand View Research, the global hydraulic press market reached about USD 15.3 billion in 2023. Forecasts differ.
Regional costs depend on tooling, freight, power, and service. A basic H-frame may appear inexpensive, yet installation, oil filtration, and dies can add 20–40% to project cost. This estimate is not universal. A 1,000-ton press may require reinforced foundations and lengthy commissioning. Suppliers should disclose cycle time, pressure stability, spare-part lead times, and acceptance-test methods.
MarketsandMarkets identifies automation and energy efficiency as major manufacturing investment themes. Variable-displacement pumps and servo controls can reduce idle losses, but savings depend on duty cycle. The International Energy Agency reports that industry consumed roughly 37% of global final energy in 2022. Therefore, buyers should compare kilowatt-hours per cycle, not motor horsepower alone. Local technicians matter more than polished brochures. Sometimes, the cheapest quote becomes the slowest asset.